5 catalogued sizes, cast to ASTM A351 CF8M. Pick any row and the technical drawing redraws to it.
Radial Compressor Wheel to ASTM A351 CF8M are catalogued in outer diameter Ø80 to Ø200, with width 32-80 mm, bore 18-44 mm, hub diameter 36.8-92 mm. 5 sizes are held in the table below, and the technical drawing redraws to whichever row you select.
Specification
ASTM A351 CF8M
Alloys
CF8M, CA6NM, CD3MN (2205)
Size range
Ø80-Ø200
Wide
32-80 mm
Catalogued sizes
5
Dimensions are nominal casting dimensions before machining allowance. Confirm the tolerance grade and the machined features against your drawing before ordering.
Alloys & Grades
The Radial Compressor Wheel is cast in 9 of the 63 grades we work in. Those are listed first; the full reference tree is underneath, with each designation shown alongside its ASTM/UNS, EN and GB equivalents.
CF8Mcatalog gradeASTM A351 CF8M / UNS J92900 (cast 316)
CA6NMASTM A743 CA6NM / UNS J91540
CD3MN (2205)ASTM A890 Gr 4A / UNS J92205 (cast 2205 duplex)
CE3MN (2507)ASTM A890 Gr 5A / UNS J93404 (cast 2507 super duplex)
C83600 Red BrassASTM B584 C83600 · UNS C83600 · 85-5-5-5
C87600 Silicon BrassASTM B584 C87600 · UNS C87600
C86300 Manganese BronzeASTM B584 C86300 · UNS C86300
Aluminum Alloy Castings
A356 / A356-T6ASTM B26 A356 · UNS A13560 · AlSi7Mg0.3 · EN AC-42000
A357ASTM B26 A357 · UNS A13570 · AlSi7Mg0.6
355 / C355ASTM B26 355 · UNS A03550 · AlSi5Cu1Mg
A201-T7ASTM B26 A201 · UNS A02010 · AlCu4MgTi
Titanium Castings
Ti-6Al-4V (Grade 5)ASTM B367 Gr C-5 · UNS R56400 · TC4 · Ti-6-4
CP Titanium Grade 2ASTM B367 Gr C-2 · UNS R50400
Special & Wear Alloys
Ni-Resist D-2ASTM A439 D-2 · UNS F43000
High-Chrome White IronASTM A532 Class III · 25Cr white iron
Technical Drawing
Every parameter below is editable, and the drawing redraws to match the values you choose. Picking a size snaps the other fields to that size's values; you can then override any one of them.
Sends the selected values to the quote form below.
Request a Quotation for Radial Compressor Wheel
The form below follows the current drawing configuration. Change the values above and the request updates with them. Attaching a drawing or a STEP file is the fastest route to a firm price.
Dimensions & Parameters (ASTM A351 CF8M)
Nominal casting dimensions before machining allowance. Every row is a starting point for the customizer above — pick any size and the drawing redraws to it.
Size
Outer Diameter ØD (mm)
Overall Width W (mm)
Bore Diameter Ød (mm)
Hub Diameter ØD1 (mm)
Blade Thickness T (mm)
Blade Count
Fillet Radius R (mm)
Casting Weight (kg)
Ø80
80
32
18
36.8
3
13
2.5
0.35
Ø100
100
40
22
46
3.2
13
2.5
0.69
Ø125
125
50
28
57.5
4
13
3
1.34
Ø160
160
64
36
73.6
5.1
13
4
2.81
Ø200
200
80
44
92
6.4
13
5
5.49
The Radial Compressor Wheel (ASTM A351 CF8M) is a high-temperature casting cast to near-net shape by the lost wax process. The complete parameter table is below, together with the alloys the part is supplied in and the tolerances held.
What Is a Radial Compressor Wheel?
The Radial Compressor Wheel is a high-temperature casting. It is selected by outer diameter together with the wall thickness and the hole or port geometry shown in the table below, and is supplied in a range of alloys and surface conditions to suit the service.
How This Part Is Cast
A wax pattern is injected, assembled onto a runner and shelled in silica sol, then dewaxed and fired before pouring under vacuum. Vacuum melting is what makes the reactive and high-nickel grades castable at all: poured in air they gas and oxidize, and the resulting inclusions are exactly the defects that shorten creep life at temperature.
Alloy Options
The catalog specification calls for CF8M. This part is supplied in CF8M, CA6NM, CD3MN (2205), CE3MN (2507), HK30, HK40, Inconel 625 (CW6MC) and A356 / A356-T6. The alloy drives both price and lead time more than any other choice on the RFQ, so state it if your drawing calls one out — and if it does not, describe the service (the medium, the temperature and the pressure) and we will propose one.
Tolerances, Finish & Machining
As-cast dimensions are held to ISO 8062-3 DCTG 6-8 on a silica sol shell, which is roughly ±0.3 mm on a 50 mm feature and widens with size. As-cast surface finish is typically Ra 3.2-6.3 µm. A machining allowance of 1.5-3 mm is added to the faces called out on the drawing; every other surface is supplied as-cast. The bore and the hub face are machined and, where the drawing calls for it, held concentric within the runout stated on it. State the tolerance grade and the finish you need on the RFQ — both change the price, and a tolerance nobody asked for is the most common avoidable cost on a casting.
Inspection & Testing
Chemical composition by spectrometer on every heat, with the certificate supplied against the specified grade.
Dimensional inspection against the drawing, with a first-article report on new tooling.
Dynamic balancing to the grade stated on the drawing (commonly ISO 1940 G6.3 for pump and fan duty).
Verification of the heat-treatment condition and, on request, elevated-temperature mechanical testing.
The Radial Compressor Wheel is made to order. Pricing starts from approximately US$38.00 per piece for the smallest listed size in CF8M at production quantity; the final figure depends on pour weight, alloy, machining scope, surface finish and order quantity, and tooling is a separate one-time charge. Submit the configuration above for a firm quotation.
Inside the plant
Manufactured in our own plant
This part is cold-formed, threaded, heat-treated and finished in-house. The stages below are where its class and finish are actually decided.
01
Tooling & wax injection
An aluminum die is cut from your drawing or 3D model, and wax is injected into it under pressure. Everything downstream is a copy of this pattern, so the die is where the tolerance is actually decided — not on the shop floor afterwards.
First-article dimensional report on every new die before production wax is run.
02
Tree assembly & gating
Patterns are welded onto a wax runner to form a tree. How they are gated is not cosmetic: the gate positions decide which sections solidify last, and a heavy section fed from the wrong direction is where shrinkage porosity comes from.
Gating reviewed against the part's heaviest section before the first tree is built.
03
Ceramic shell building
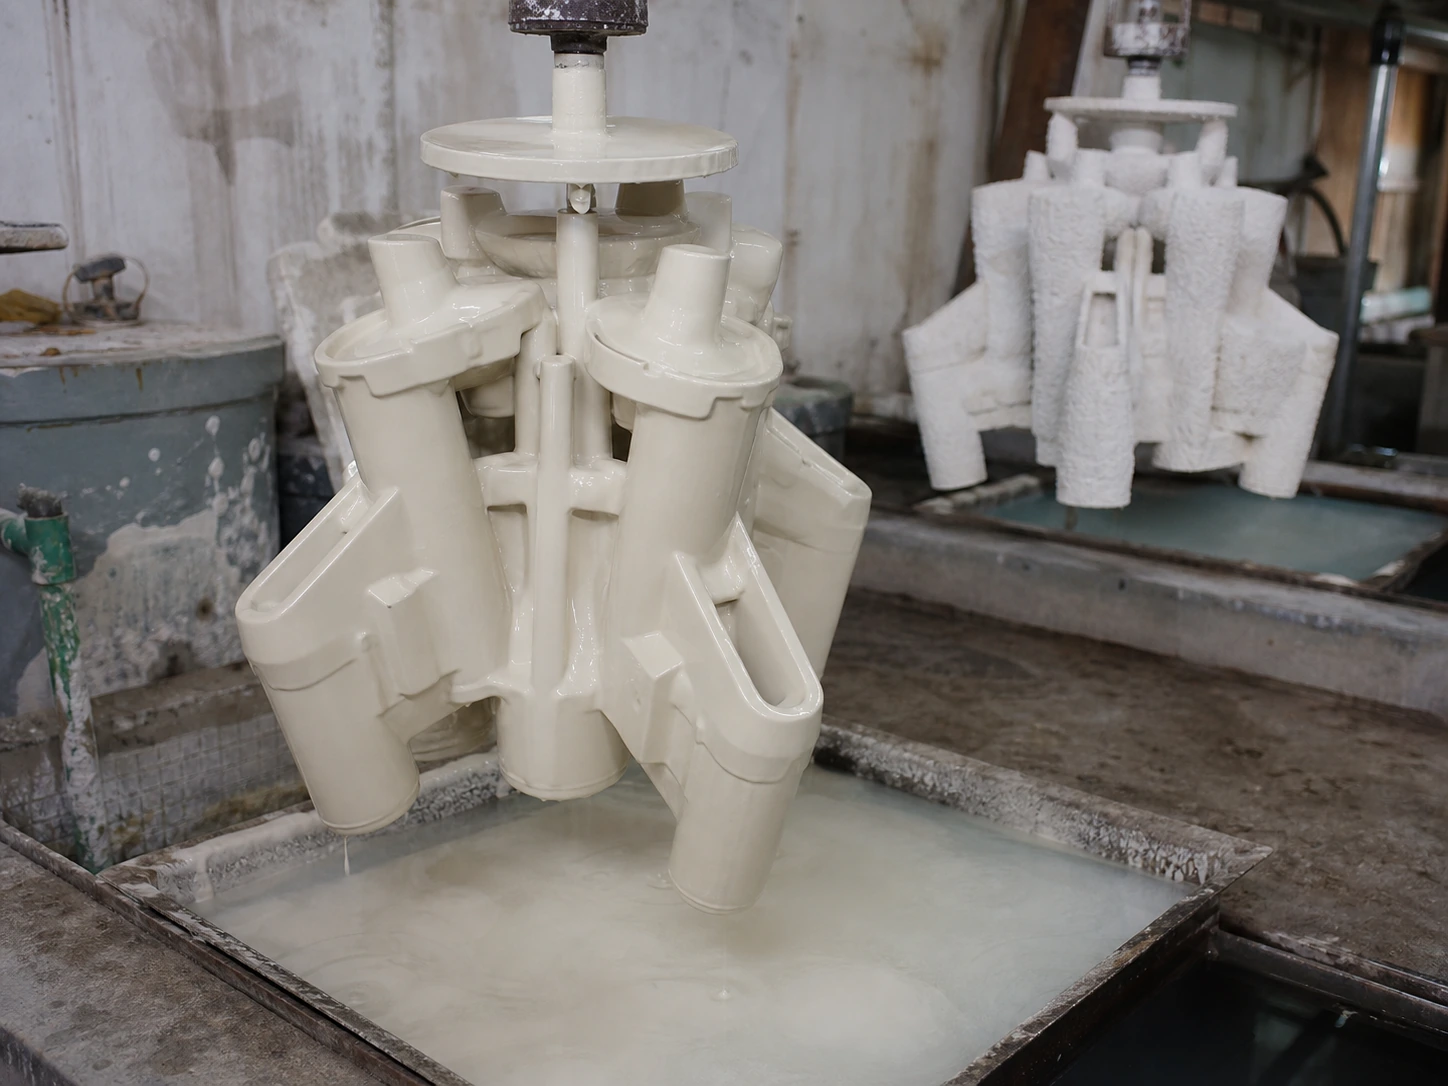
The tree is dipped in ceramic slurry and stuccoed with refractory grain, six to eight times, drying between coats. The face coat is what the casting surface copies, which is why a silica sol face gives Ra 3.2-6.3 µm where a water-glass shell gives a coarser one.
Slurry viscosity and drying room temperature and humidity logged per coat.
04
Dewaxing
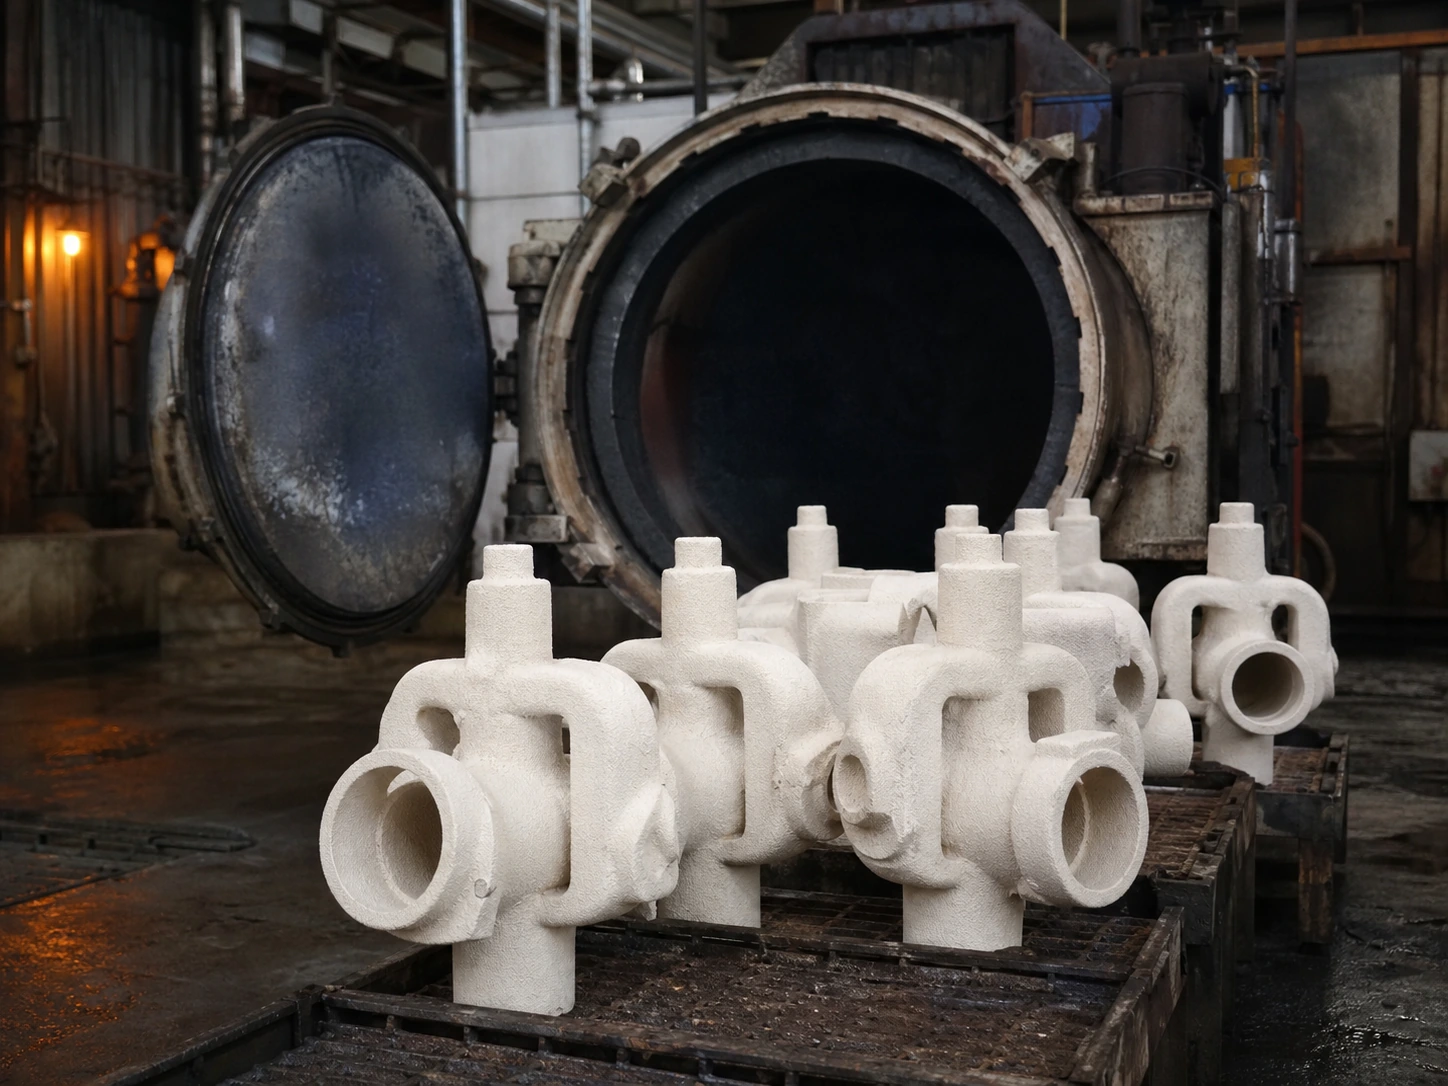
A steam autoclave melts the wax out fast, so that the wax — which expands more than the ceramic does — leaves before it can split the shell. Recovered wax is filtered and reused for gating rather than for patterns.
Every shell inspected for cracks after dewax; a cracked shell is scrapped, not patched.
Video: Radial Compressor Wheel
Third-party video, selected automatically for this topic. It is not produced by Lost Wax Casting and is not a specification source — use the tables on this page for dimensional data.
Frequently Asked Questions
What standard is the Radial Compressor Wheel cast to?
The Radial Compressor Wheel is cast to ASTM A351 CF8M. The dimensions on this page follow that specification, and the material certificate supplied with the order is issued against it.
What is the size range of the Radial Compressor Wheel?
The table on this page lists 5 sizes for the Radial Compressor Wheel by outer diameter, from Ø80 to Ø200. Sizes outside the table are quoted on request — investment casting is tooled per part, so a new size is a new pattern die rather than a stock item.
Which alloys is the Radial Compressor Wheel cast in?
The catalog specification calls for CF8M. The Radial Compressor Wheel is supplied in CF8M, CA6NM, CD3MN (2205), CE3MN (2507), HK30 and HK40. The alloy drives both the price and the lead time more than any other choice on the RFQ, so state it if your drawing calls one out — and if it does not, describe the service (the medium, the temperature and the pressure) and we will propose one.
What wall thickness does the Radial Compressor Wheel have?
The listed sizes run from 3 mm to 6.4 mm of nominal wall. Investment casting will hold a section down to about 1.5 mm in the silica sol shell used here — 0.6 mm on a small isolated feature — and the thin end of that range is a shell-filling question rather than a strength one. A section much heavier than the surrounding wall is the more common problem: it solidifies last and shrinks, so it is fed or cored rather than left solid.
Is the Radial Compressor Wheel dynamically balanced?
The Radial Compressor Wheel rotates in service, so it is balanced to the grade stated on the drawing — commonly ISO 1940 G6.3 for pump and fan duty, and tighter for high-speed work. Balance is done after the bore and the hub face are machined, because those are the datums the balance is measured against.
How do I request a quotation?
Set the configuration on the technical drawing above — size, alloy, finish — and click "Request this configuration". The values carry into the quote form below it. Attach a drawing or a STEP file if you have one; it is the fastest route to a firm price, and it lets us flag any castability issue before you commit to tooling.
Guides for the Radial Compressor Wheel
Each grade changes the price, the weight and what the part survives, so there is a page per grade for this part: CF8M (the catalog grade), HK30 (for exhaust-gas temperature), HK40 (creep strength in furnace duty), CA6NM (tough and cavitation resistant), CD3MN (2205) (roughly double the yield strength) and CE3MN (2507) (super duplex, for warm seawater).
How it is shelled decides the tolerance and the surface you get, and the tolerance band is worked out against this part's own dimensions on each: Vacuum Investment Casting (DCTG 5 – 7, Ra 3.2 – 6.3 µm).
The specification and the testing change by sector more than the geometry does, so the radial compressor wheel is written up separately for Power Generation, Oil & Gas and Aerospace & Defense.
If the question is still whether a casting is the right way to make this part at all, the Radial Compressor Wheel application guide covers where it is used, what has to be decided before a price exists, and where investment casting is the wrong answer.
Need a casting quote or a castability review?Message our engineers on WhatsApp — send a drawing or DIN number and get pricing back fast.Start WhatsApp Chat →
This website uses only necessary and functional cookies to operate, secure, and improve basic website performance.
We do not use advertising cookies, Google Analytics, or cross-site tracking technologies.
Privacy Policy